Quality
We Ensure Our Valves Meet Global Standards
If you require reliable, high-performance valves, our QA team is here to ensure your project's success.
Using Coordinate Measuring Machines (CMMs), high-pressure multi-media test benches, and metallurgical laboratories, our valves undergo 100% inspection with full traceability — giving you the confidence to meet strict specifications, reduce approval risks, and comply with API, ANSI, ISO, and customer-specified standards.
Each valve features a unique serial number linked to its production records, inspection data, and final test reports — ensuring full transparency, auditability, and traceability of materials and inspection information throughout your entire project lifecycle.
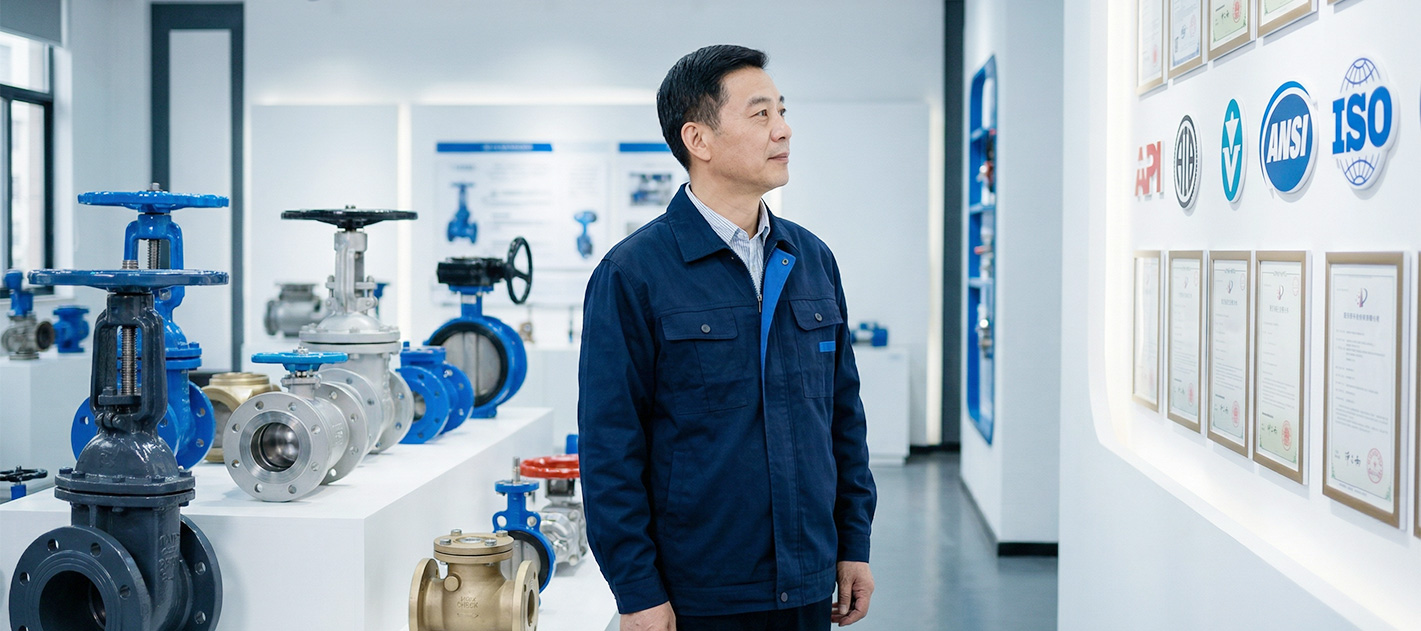
Every Tested Valve Is Field-Ready for Your Project
01
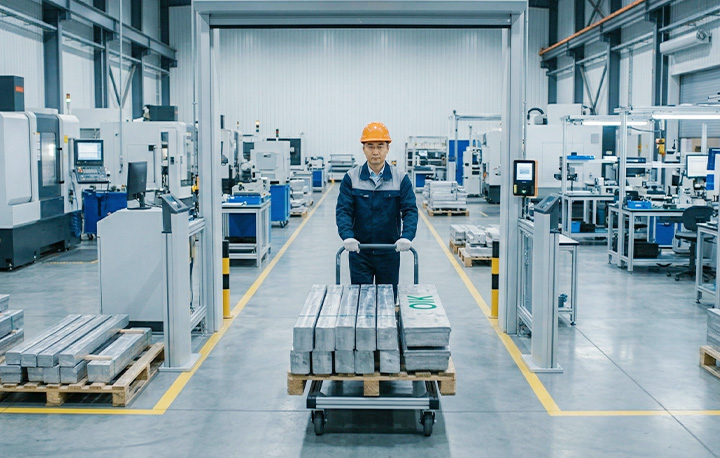
Incoming Material Inspection
Using spectrometers, tensile testing machines, and hardness testers, we verify the chemical composition, mechanical strength, and material origin prior to production.
Only qualified materials enter your production workflow — helping you avoid downstream failures, premature corrosion, and pressure rating-related risks from the very beginning.
02
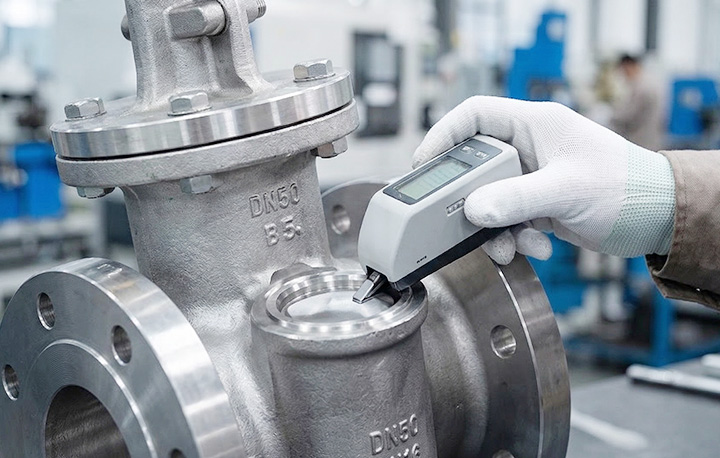
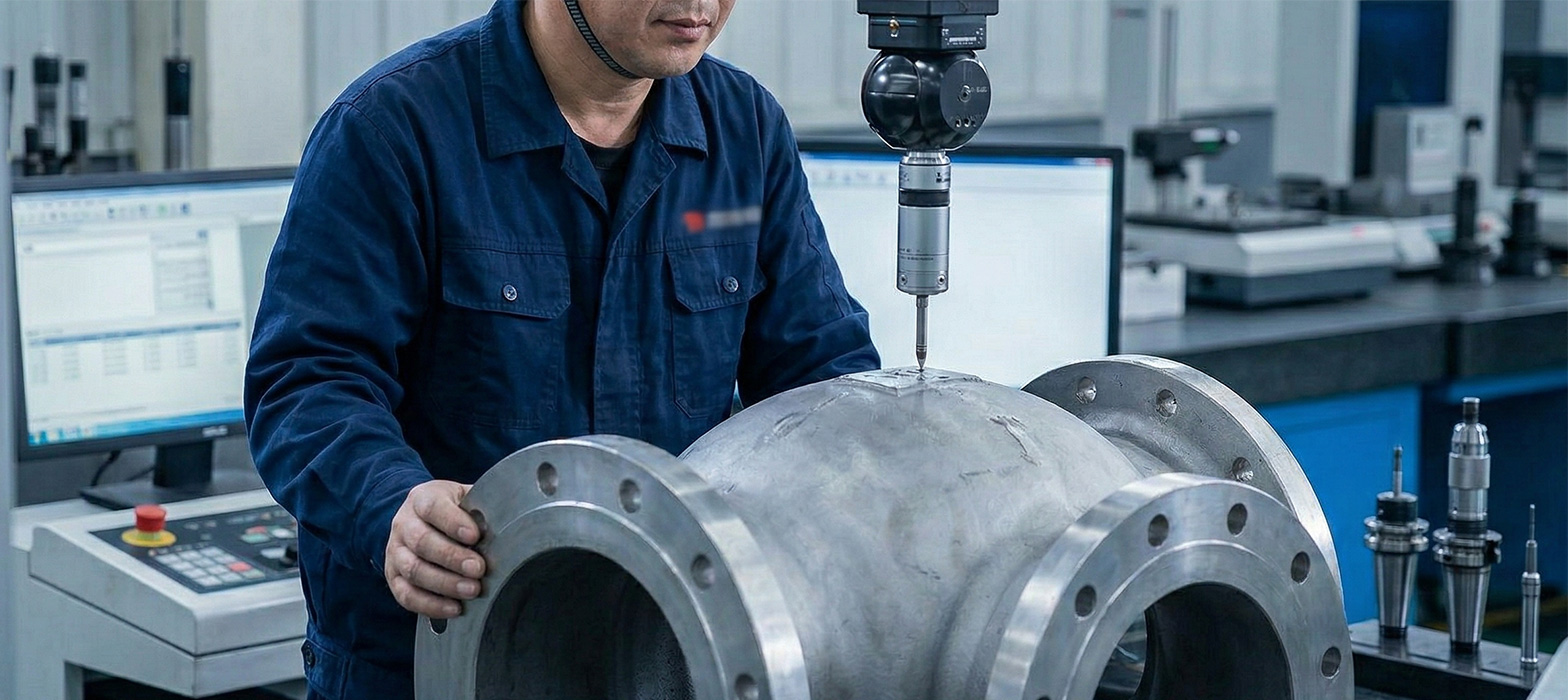
In-Process Dimension & Precision Inspection
CMM systems, optical measurement equipment, surface roughness meters, and calibrated calipers monitor your valves’ critical sealing faces and assembly tolerances throughout machining and fabrication.
This ensures true interchangeability, accurate fitting, leak-free assembly, and fewer alignment issues when your valves reach the installation site.
03
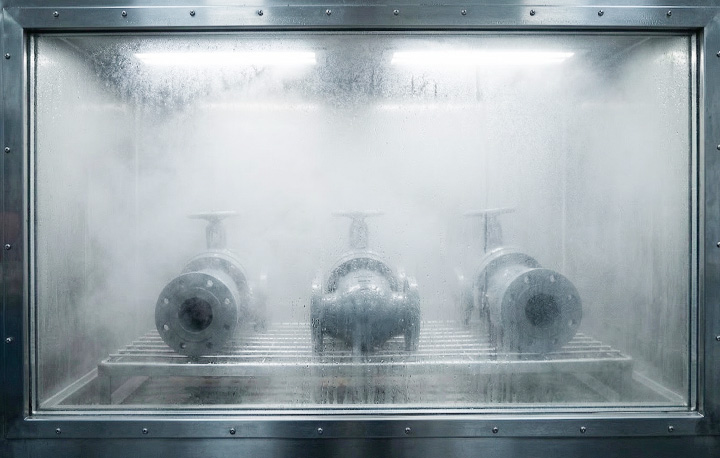
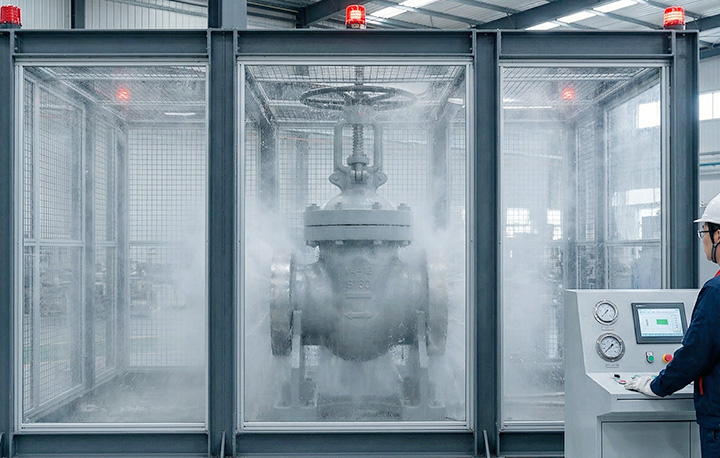
Surface & Corrosion Testing
Through salt spray chambers and coating-thickness gauges, we validate coating adhesion and corrosion protection performance.
Your valves are verified to withstand harsh conditions in chemical processing, marine service, power plants, and offshore environments — extending service life where failure is least tolerable.
04
Functional & Pressure Testing
Multi-media hydrostatic & pneumatic test stations, leak detection systems, and endurance test rigs verify:
- Body strength
- Sealing integrity
- Operational endurance through cycle testing
Every valve leaves our factory certified compliant with API, ANSI, and customer-specific performance requirements.
Complete Inspection Documentation
With every shipment, you receive a full inspection paperwork package, including:
- 170+ Mazak machines enable precise, efficient valve production
- 36+ CNC machining centers ensure ±0.005 mm repeatability
- 1,000,000+ valves produced annually for global industrial projects
- 15–25 days standard orders delivered on predictable schedule
These documents support your EPC submittals, third-party audits, government inspections, and final acceptance processes — saving weeks of clarification and approval time while keeping your project schedule intact.
Continuous Quality Improvement
Beyond individual inspections, your supply quality is continuously protected through systemic control:


This ensures your valve supply remains stable, compliant, and continuously optimized — even across large volumes and urgent project schedules.
Before & After Your Order
Full-Cycle Valve Assurance
From selection to long-term operation, everything is built to protect your installation, compliance, and uptime.
Accurate Valve Selection You Can Trust
- 100+ valve types supported — Gate, Globe, Check, Ball & Butterfly valves for engineering matching.
- Certified compliance coverage — API 6FA, CE, SIL & Special Equipment Type Tests for tender and inspection approval.
- Real-service condition validation — Proven support for nitric acid & phosphoric acid media, -196–816°C temperature range, and PN10–PN320 pressure classes.
- Open factory qualification review — Direct verification of our ISO9001 quality management certifications before order placement.
Continuous Project Support
- All production is controlled under the ISO 9001:2015 quality management system.
- We have established proven supply chain service workflows through long-term cooperation with major industrial clients, including China National Chemical Corporation and China Huadian Corporation.
- On-demand technical support — providing installation guidance, troubleshooting, performance evaluation, and operational advice throughout the entire lifecycle of your valves.
- Traceable product service support — Your valve's serial number enables instant retrieval of production history, inspection records, and test data when post-delivery verification or service support is required.